
2026年11月10日
Discover casting traceability and industrial IoT monitoring for smarter production quality control real time data and improved efficiency
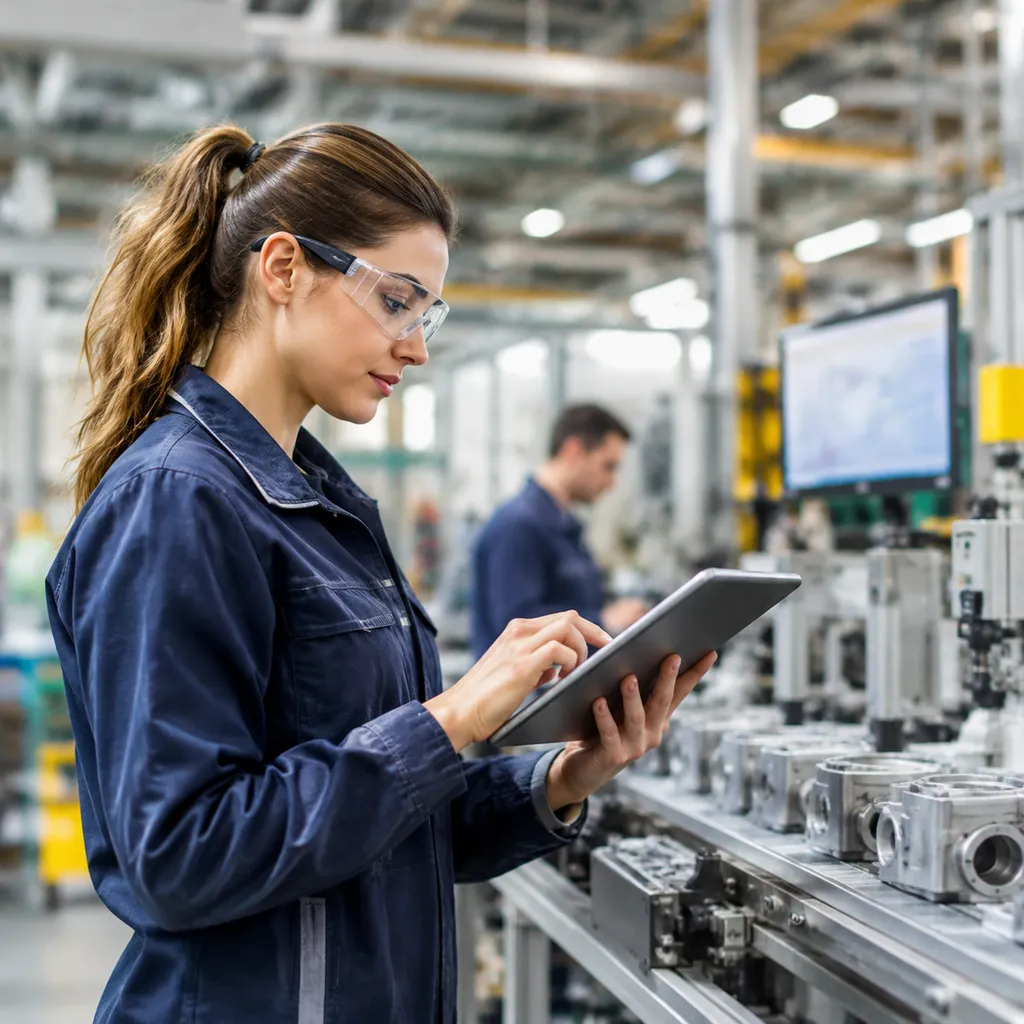
Core Pillars of Casting Traceability and Industrial IoT Monitoring
Modern foundries can no longer rely on clipboard logs and post-mortem quality checks. Porosity, inclusions, and dimensional shifts demand immediate, data-backed intervention at the pour line. We built our framework on three structural pillars to bridge physical metallurgical operations with real-time digital intelligence, delivering end-to-end Casting Traceability and Industrial IoT Monitoring.
Unique Digital Part Genealogy from Melt to Finish
Tracking batches at the heat level is insufficient for high-spec manufacturing. We assign a unique digital thread for metal casting to every individual component, tracking it continuously through its lifecycle.
- Direct Part Marking (DPM): High-contrast 2D matrix or laser-etched identifiers applied directly to raw castings post-shakeout.
- Melt Chemistry Correlation: Instant linking of optical emission spectrometry (OES) chemical compositions directly to the unique serial ID.
- Thermal History Archival: Granular logging of ladle tap temperatures, inoculation timing, and liquidus-to-solidus cooling curves.
- Secondary Operations Logging: Automatic attachment of heat treatment batches, shot blasting, and CNC machining records to the core ID.
| Traceability Milestone | Data Captured | Shop-Floor Impact |
|---|---|---|
| Melt & Inoculation | Spectro chemistry, tap temperature, alloy weights | Prevents off-spec chemistries from pouring |
| Mold Filling | Pour duration, gating velocity, pyrometer curves | Eliminates misruns and cold shuts |
| Shakeout & Finishing | Cooling time, shot-blast cycle, operator ID | Validates stress relief and mechanical integrity |
Real-Time Process Parameter Synchronization Across Molds
Isolated machine metrics hide active defects. Our system synchronizes dynamic pouring parameters with specific mold cavities in sub-second intervals to verify process compliance before the metal solidifies.
- Dynamic Pressure & Temperature Curves: Continuous monitoring of cavity pressure and mold wall thermal gradients via embedded sensors.
- Automated Tolerance Verification: Immediate flagging when pour speed or ladle approach angles breach engineering limits.
- Mold Cavity Mapping: In multi-cavity dies, telemetry maps defect clusters directly to specific tooling wear patterns.
Edge-to-Cloud Infrastructure for Zero Data Latency
Harsh foundry environments cannot tolerate cloud-dependent latency or lost connectivity during critical operations. We deploy a hybrid edge-to-cloud computing layer to process data where the metal pours.
- Millisecond Edge Processing: Ruggedized edge gateways capture high-frequency telemetry from pyrometers and flow meters, executing anomaly detection in under 10 milliseconds.
- Local Autonomous Buffering: In the event of network disruption, local gateways buffer up to 30 days of raw operational telemetry without data loss.
- Bi-Directional Cloud Sync: Clean, contextualized datasets stream securely to the central data lake via MQTT and OPC-UA protocols for enterprise-wide visibility and cross-facility benchmarking.
Technical Features of the Vastpe IIoT Monitoring Platform
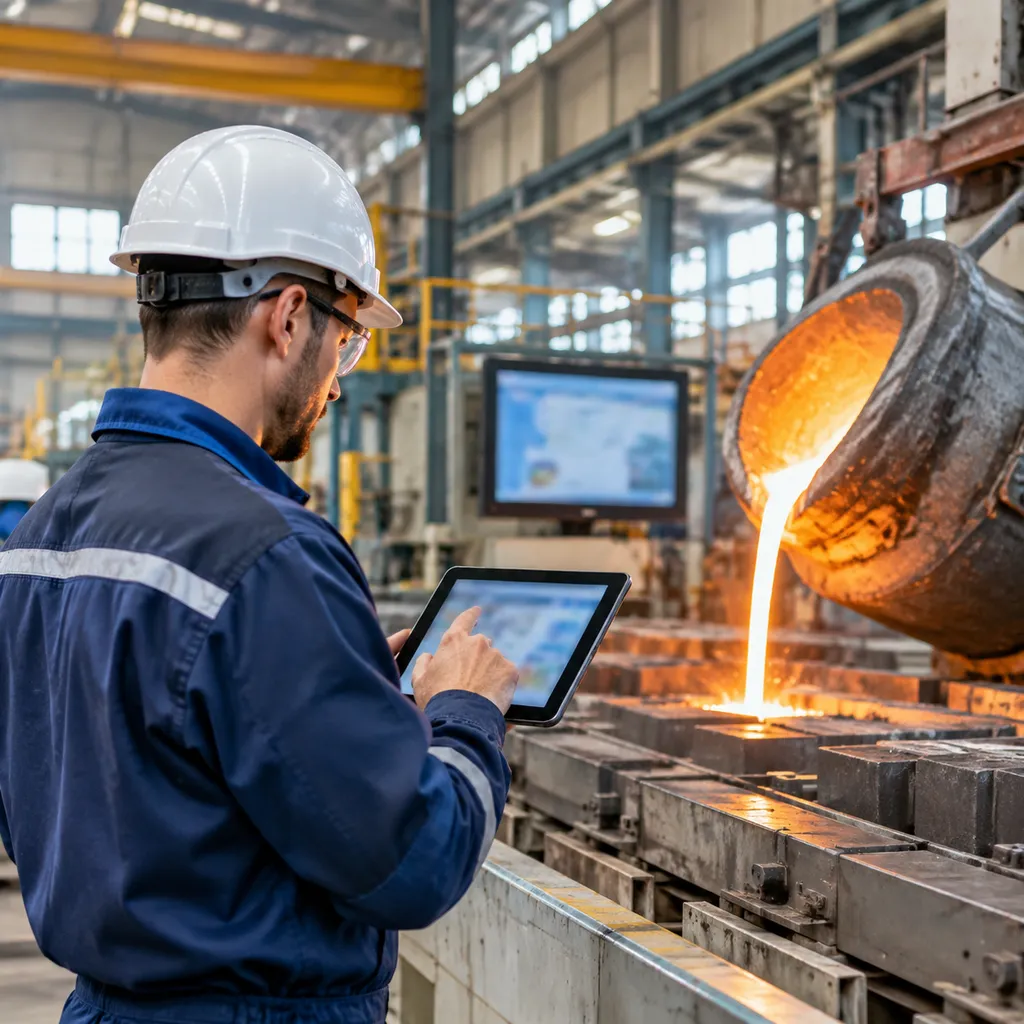
We engineered our platform to eliminate blind spots on the foundry floor. By bridging low-latency sensory hardware with edge analytics, our Casting Traceability and Industrial IoT Monitoring architecture captures critical metallurgical metrics at the millisecond level, turning raw pouring dynamics into actionable quality controls.
Multi-Point Thermal, Pressure, and Pour Speed Sensing
Process variation during pouring is the primary driver of scrap. We deploy ruggedized, non-contact infrared pyrometers and quartz pressure transducers directly at ladles, runners, and mold cavities. Thermal tracking: Continuous capture of melt superheat, mold surface temperature, and cooling curves. Flow dynamics: Real-time pour velocity and mold-filling backpressure metrics to detect turbulent flow instantly. Environmental compensation: Auto-calibrated sensors rated for continuous operation above 1,200°C ambient exposure.
Native Legacy PLC, SCADA, and OPC-UA Integration
Foundries cannot afford to rip and replace operational machinery. We bridge legacy hardware and modern analytics through native edge protocols: Protocol support: Out-of-the-box drivers for Siemens, Allen-Bradley, Modbus TCP, and OPC-UA casting data integration. Zero machine downtime: Non-invasive tap connections capture analog and digital signals without halting active production lines. Synchronized data ingestion: High-frequency machine telemetry aligns directly with mold IDs and pour batches.
| Layer | Technical Spec | Core Metric Tracked |
|---|---|---|
| Edge Sensing | Multi-channel thermocouple & piezoresistive arrays | Pour temperature, fill rate, cavity pressure |
| Connectivity | Industrial Gateway via OPC-UA / MQTT | PLC cycle times, gate open/close signatures |
| Analytics Engine | Embedded ML pattern inference | Cooling gradient drift, gas entrapment risk |
| Data Record | Immutable digital ledger | Serialized part genealogy, operator sign-offs |
AI-Powered Pattern Recognition for Casting Defects
Our machine learning models evaluate thermal gradients and fill speeds in real time against historical defect libraries. When a pour deviates from the target threshold, the system flags the specific mold before it ever reaches the shakeout table. This automated defect tracking pinpoints risks like shrinkage porosity, cold shuts, and slag inclusion before downstream machining costs accrue.
Automated Compliance Logs and Digital Audit Trails
Paper logs create liability. We replace manual record-keeping with automated, time-stamped digital threads tied directly to strict casting quality standards for reliable metal parts. Every serialized casting captures: Exact chemistry and spectrometer readings from the melt heat. Pour-by-pour cooling rates and ambient humidity logs. Non-destructive testing (NDT) results mapped to individual heat numbers.
This end-to-end data captures full production accountability, making external quality audits fast and indisputable.
Operational Benefits and Scrap Reduction in Foundries
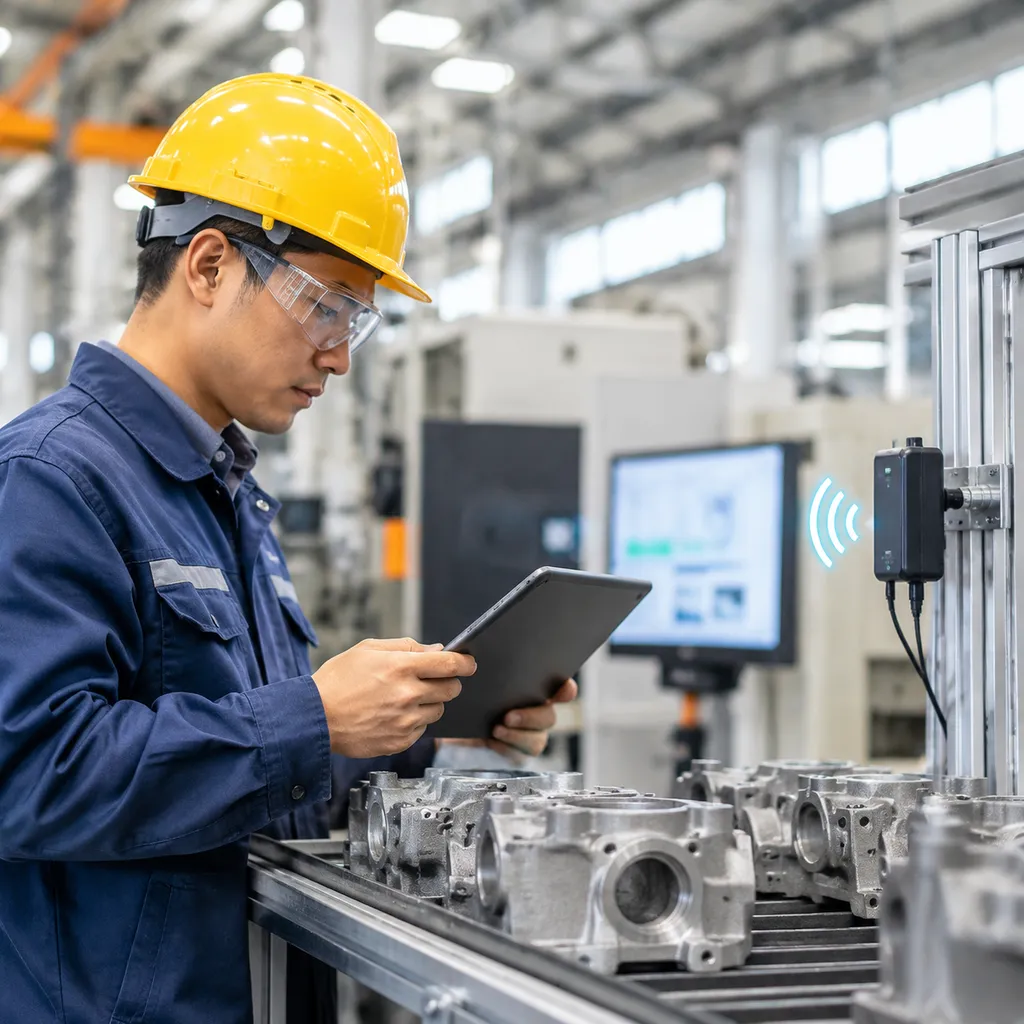
By implementing our Casting Traceability and Industrial IoT Monitoring architecture, foundries replace guesswork with hard telemetry. We attack scrap generation at the source while insulating operations against downstream liability and costly customer chargebacks.
| Metric | Legacy Foundry Operations | Vastpe IIoT & Traceability | | Defect Detection | Post-machining / Final NDT | In-process & Real-time | | Scrap Rate Avg | 6% – 12% baseline | Reduced by 25% – 40% | | Audit Prep Time | 3–5 days (manual paper logs) | Instant (1-click digital) | | Unplanned Furnace Stop | Reactive repair upon failure | Predictive alerts via IIoT |
Real-Time Alerts to Prevent Thermal Drift and Porosity
Molten metal quality hinges on tight thermal and atmospheric windows. Our real-time casting process monitoring detects pouring temperature anomalies, cooling rate deviations, and mold filling irregularities the second they cross critical thresholds.
- Instant Threshold Traps: We trigger audible and mobile push notifications when melt temperatures drop outside metallurgy specifications, stopping scrap before the next mold indexes.
- Porosity Mitigation: Correlating ambient humidity, gating pressures, and pour speeds eliminates entrapment defects and gas porosity across batch runs.
Root-Cause Analysis Driven by Serialized Batch History
When a defective part surfaces at final machining, tracing its origin typically takes days of manual log sorting. Our casting genealogy software gives every casting an indelible digital fingerprint:
- Serialized Part Tracking: Laser-marked 2D matrix codes link individual castings directly to furnace heat numbers, ladle fill sequences, and core mold pressures.
- Targeted Containment: If a metallurgy or cooling anomaly occurs, we isolate the exact 15 affected castings instead of scrapping an entire 500-unit heat treat lot.
Audit-Ready Compliance for Tier-1 Automotive and Aerospace Specs
Stringent quality standards like IATF 16949 and AS9100 demand end-to-end data integrity. We automate this record-keeping to provide foolproof proof of conformance. For critical applications—including structural components and high-integrity titanium investment casting for aerospace and medical parts—our platform records every thermal profile and chemist validation directly into non-editable, audit-ready compliance logs.
Furnace Uptime Optimization and Lower Liability Risks
Foundry margins hinge on energy management and melt asset reliability. We apply predictive maintenance for casting furnaces to prevent unscheduled downtime:
- Lining Degradation Tracking: Multi-point thermal sensors continuously calculate induction furnace refractory wear to stop runouts before catastrophic failures.
- Power Consumption Analytics: Continuous load tracking pinpoints slag buildup and inductor degradation, reducing kWh per ton melted.
- Legal & Recall Protection: Stored digital batch records verify that defective parts returned from the field either met customer engineering specs upon release or originated from an unmonitored supplier batch.
Step-by-Step Implementation Roadmap for Foundries
Deploying casting traceability and Industrial IoT monitoring does not require shutting down your foundry or replacing functional legacy assets. We execute rollouts using a phased, non-invasive deployment model designed around active production cycles.
[Phase 1: Sensor Retrofit] ➔ [Phase 2: Edge Aggregation] ➔ [Phase 3: Analytics & Alerts] (Day 1 - 10) (Day 11 - 20) (Day 21 - 30)
Phase 1: Sensor Retrofitting and Non-Invasive Hardware Placement
We begin directly at the floor level by installing hardened instrumentation across key thermal and mechanical choke points:
- Non-Invasive Sensing: We mount split-core current transformers on melt deck induction lines and install optical pyrometers above pour cups without drilling into structural machine frames.
- Process Synchronization: Sensors are placed systematically across core molding, melting, and shakeout zones. Integrating sensors across every milestone detailed in our casting process guide on methods and key steps guarantees uninterrupted telemetry from raw charge to final shakeout.
- Direct Identification Tagging: We install direct part marking (DPM) stations and laser markers at mold knockouts to affix serial heat-tracking IDs the moment components exit the line.
Phase 2: Industrial Gateway Setup and Data Aggregation
Raw telemetry is useless if it stays isolated on the plant floor. In this stage, we tie disparate machine signals into a unified Foundry 4.0 data stream:
- Protocol Bridging: We connect field sensors, older relay-logic panels, and modern PLCs to industrial edge gateways running OPC-UA, MQTT, Modbus TCP, and Profinet protocols.
- Edge Data Cleaning: Edge devices filter electrical noise, timestamp millisecond-level pour data, and buffer readings locally. This prevents data gaps during plant-wide network interruptions.
- Genealogy Mapping: The edge layer links ladle metallurgical chemistry, batch heat numbers, and individual mold IDs into an immutable digital record before sending packets to the server.
| Deployment Phase | Primary Hardware Deployed | Protocols / Standards | Key Target Deliverable |
|---|---|---|---|
| Phase 1: Retrofit | Optical pyrometers, IR sensors, laser markers | Modbus RTU, 4-20mA, IO-Link | Zero-downtime sensor attachment |
| Phase 2: Aggregation | Edge gateways, network switches | OPC-UA, MQTT, Profinet | Clean, synchronized data ingestion |
| Phase 3: Dashboard | Local servers, secure cloud instances | REST APIs, WebSockets | Live genealogy & automated scrap alerts |
Phase 3: Central Dashboard Configuration and Alert Tuning
The final stage transforms raw field metrics into operational control:
- Dynamic Alarm Thresholds: We set variable upper and lower control limits for pour temperatures, mold cooling curves, and fill times based on specific alloy metallurgy.
- Floor-Level Alerting: High-temperature excursions or pour-speed drop-offs trigger instant SMS, stack light, and HMI warnings, allowing pour teams to abort bad fills before producing non-conforming batches.
- Operator Dashboard Calibration: We tailor screens specifically for foundry supervisors and quality inspectors, displaying live heat genealogy, mold cavity status, and real-time scrap indicators on a single screen.
Frequently Asked Questions About Casting Traceability and IIoT
Modernizing your facility through Casting Traceability and Industrial IoT Monitoring often raises practical concerns regarding implementation and durability. We address these common operational questions to help you streamline your digital transition.
How do IoT sensors survive extreme casting furnace environments?
Our sensors utilize industrial-grade, hardened housings designed for high-temperature resilience. We implement non-invasive mounting strategies and thermal shielding to ensure hardware longevity, even when monitoring heat treatment furnace for castings with 5c uniformity or volatile pouring zones.
Can this traceability software interface with older foundry machinery?
Yes. Our platform features universal gateway support, allowing us to bridge data from legacy PLC, SCADA, and analog machine controllers. We translate disparate signals into a unified data stream without requiring you to replace your existing assets.
How does digital genealogy help reduce scrap rates?
By creating a unique digital thread for every part, we correlate specific melt and pour parameters with the final product quality. When a defect occurs, our system performs an automated root-cause analysis, identifying if the issue stemmed from thermal drift or speed inconsistencies, allowing you to rectify the process immediately.
What is the expected ROI timeline for foundry IoT retrofits?
Most facilities realize a positive ROI within 12 to 18 months. By minimizing scrap, reducing manual audit labor, and optimizing furnace uptime, the efficiency gains typically offset the initial hardware and software investment rapidly. Consistent data visibility also prevents expensive warranty claims, further securing your profit margins.
 English
 Russian
 German