
2026年8月10日
8620 material low carbon alloy steel with high case hardness core strength heat treat response and stock options for gears shafts and fasteners
What is AISI 8620 Material?
AISI 8620 material is a low-carbon nickel-chromium-molybdenum alloy steel known for its exceptional balance of core toughness and surface hardness. In our investment casting foundry, we frequently select 8620 steel for components that must withstand heavy shock loads, cyclic stress, and severe mechanical wear.
When carburized, 8620 alloy steel develops an extremely hard, wear-resistant outer case while maintaining a ductile, fracture-resistant core.
Essential Material Characteristics
| Feature | Performance Specification | Engineering Advantage |
|---|---|---|
| Alloy Base | Nickel (Ni), Chromium (Cr), Molybdenum (Mo) | Delivers high hardenability and uniform grain structure. |
| Core Toughness | Superior impact resistance | Prevents brittle cracking under high dynamic loads. |
| Surface Wear | High case hardness (up to 58–62 HRC post-carburizing) | Resists sliding abrasion and frictional wear. |
| Fabrication | Machinability rating ~65% (B1112 standard) | Allows smooth cutting, milling, and conventional welding. |
Why Choose 8620 Investment Casting Over Wrought Forgings?
When engineering complex structural parts, technical buyers often weigh 8620 steel investment casting against standard carbon steel castings or wrought forgings.
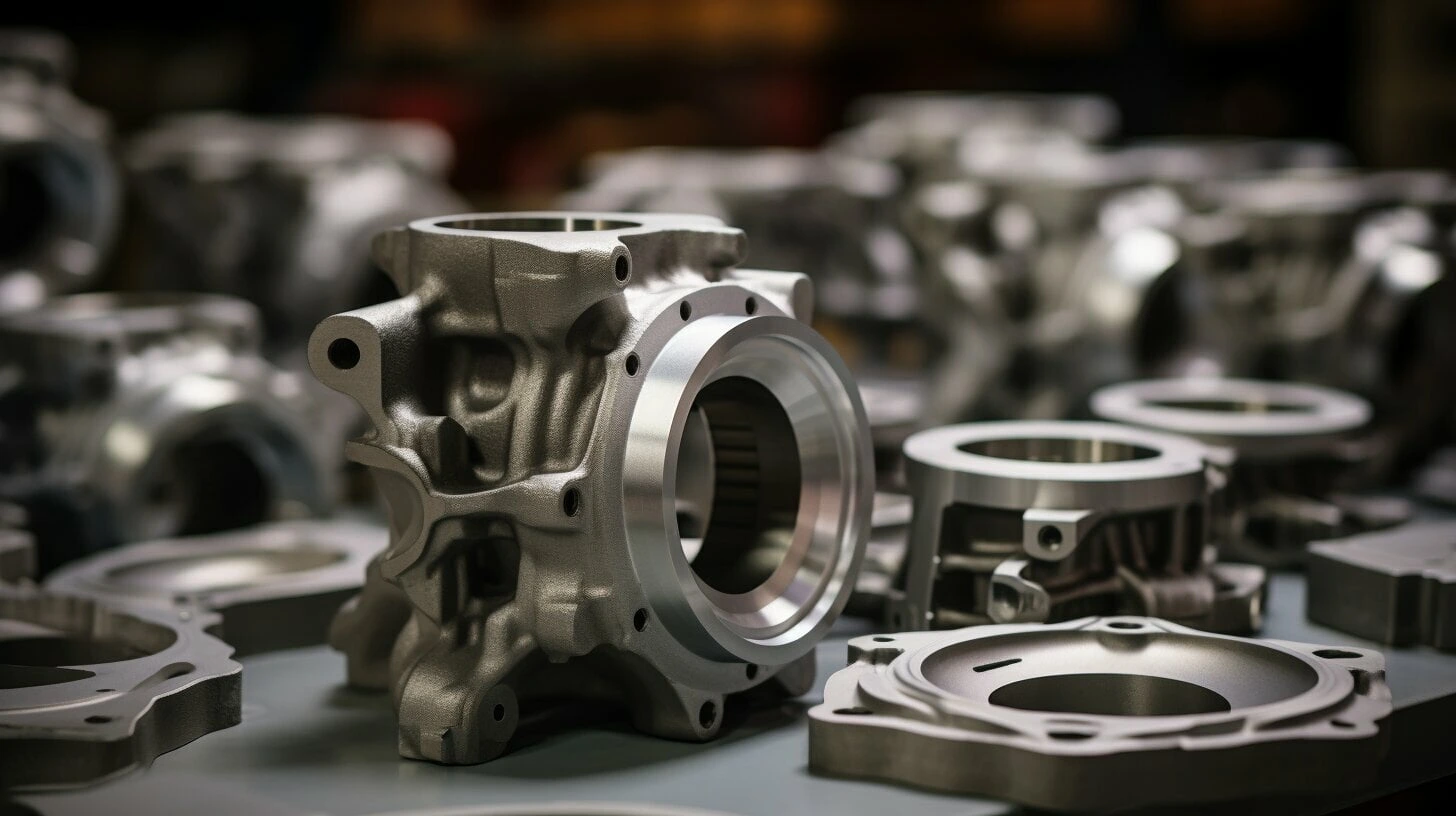
- Near-Net-Shape Precision: We cast intricate geometries directly into the component, eliminating up to 80% of secondary CNC milling operations.
- Reduced Material Waste: Wrought forging requires extensive hogging and metal removal. Precision investment casting utilizes only the metal needed for the final part design.
- Superior Alloy Performance: Standard carbon steel lacks the hardenability and fatigue resistance needed for high-stress drive components. 8620 material delivers significantly higher core strength after thermal processing.
Key Advantages of VastPCC 8620 Steel Investment Casting
How do technical buyers eliminate excessive machining costs without compromising structural integrity? We build accuracy directly into our 8620 material production through advanced tooling and strict process control. Our precision investment casting services focus on delivering consistent near-net-shape components that streamline your manufacturing workflow.
- High Dimensional Stability: Automated hydraulic wax pattern molding prevents manual deformation and guarantees lot-to-lot repeatability.
- Tight Casting Tolerances: We routinely achieve ISO 8062-3 CT5–CT7 tolerances, ensuring predictable fits for final assembly.
- Near-Net-Shape Geometry: Castings require minimal stock removal, drastically cutting down CNC turning, milling, and raw material waste.
| Quality Metric | Standard Sand Casting | VastPCC 8620 Precision Casting |
|---|---|---|
| Tolerance Standard | ISO 8062-3 CT9–CT11 | ISO 8062-3 CT5–CT7 |
| Wax Injection | Manual / Semi-Auto | Fully Automated Hydraulic |
| Machining Stock Allowance | 3.0 mm – 6.0 mm | 0.5 mm – 1.5 mm |
| Surface Finish | Ra 12.5–25 µm | Ra 3.2–6.3 µm |
AISI/SAE 8620 Chemical Composition Standard
Out-of-spec chemical chemistry ruins heat treatment response and leads to inconsistent core toughness in finished parts. We verify every melt batch against strict ASTM A29 and AISI/SAE standards to ensure our 8620 material delivers uniform hardenability and optimal carburizing performance.
| Element | Weight Percentage (%) |
|---|---|
| Carbon (C) | 0.18% – 0.23% |
| Manganese (Mn) | 0.70% – 0.90% |
| Nickel (Ni) | 0.40% – 0.70% |
| Chromium (Cr) | 0.40% – 0.60% |
| Molybdenum (Mo) | 0.15% – 0.25% |
| Silicon (Si) | 0.15% – 0.35% |
| Phosphorus (P) | ≤ 0.035% Max |
| Sulfur (S) | ≤ 0.040% Max |
- Balanced Alloy Synergy: The combination of nickel, chromium, and molybdenum in 8620 alloy steel provides predictable case-hardening depth while preserving core ductility.
- Impurity Control: We strictly cap phosphorus and sulfur limits to protect against micro-cracking, maintaining superior fatigue strength and structural integrity under dynamic shock loads.
Mechanical Properties of 8620 Alloy Steel
Will 8620 material handle high contact fatigue and heavy shock loads without fracturing? That is the standard question design engineers ask us when selecting alloys for power transmission components.
The primary advantage of 8620 alloy steel is its ability to transform significantly through thermal processing. In the as-cast or normalized state, it remains ductile and easy to machine. Once carburized and quenched, it yields a hard, wear-resistant outer shell with a tough, shock-absorbing core.
Mechanical Property Breakdown: As-Cast vs. Heat-Treated
The baseline 8620 steel material property data below compares untreated investment castings against carburized, quenched, and tempered components.
| Mechanical Property | As-Cast / Normalized | Carburized & Quenched (Core) | Carburized Case (Surface) |
|---|---|---|---|
| Tensile Strength | 520–650 MPa (75–94 ksi) | 700–980 MPa (101–142 ksi) | N/A (Surface layer) |
| Yield Strength | 350–450 MPa (50–65 ksi) | 480–690 MPa (70–100 ksi) | N/A (Surface layer) |
| Surface Hardness | 150–200 HBW | 200–300 HBW | 58–62 HRC |
| Core Hardness | 150–200 HBW | 30–40 HRC | N/A |
| Elongation at Break (%) | 20% – 25% | 15% – 20% | N/A |
| Reduction of Area (%) | 45% – 55% | 40% – 50% | N/A |
Physical and Thermal Properties of UNS G86200
When calculating structural loads, thermal expansion, or dynamic balance for cast components, we rely on these standard UNS G86200 properties:
- Density: 7.85 g/cm³ (0.283 lb/in³) — Standard mass profile ideal for accurate CAD weight calculations.
- Thermal Conductivity: 46.6 W/m·K — Efficiently dissipates friction heat across sliding surfaces like gear teeth and drive shafts.
- Modulus of Elasticity: 205 GPa (29.7 x 10⁶ PSI) — Delivers minimal elastic deformation under high torsional torque.
- Machinability Rating: ~65% (normalized, based on AISI 1212 as 100%) — Allows high cutting speeds and long tool life during preliminary CNC roughing before case hardening.
Carburizing and Case-Hardening 8620 Material
How do you achieve extreme surface wear resistance without making your finished component brittle? Through-hardening structural components often leads to catastrophic cracking under sudden shock loads. We solve this by carburizing 8620 material, transforming a low-carbon alloy into a hard-wearing, impact-resistant component.
During the thermo-chemical case-hardening process, carbon diffuses into the outer surface layer at elevated temperatures before quenching and tempering. This process gives SAE 8620 case hardening steel its signature dual-property profile:
- Surface Hardness (58–62 HRC): A high-carbon martensitic outer shell that resists extreme abrasion, scoring, and contact fatigue.
- Core Toughness (30–40 HRC): A ductile interior core that retains energy-absorption capacity to prevent sudden structural failure under dynamic loads.
- Tailored Case Depth: Controlled atmospheric processing allows us to hold precise effective case depths—typically ranging from 0.5 mm to 1.8 mm (0.020 in to 0.070 in) depending on component geometry and application requirements.
This dual-zone structure maximizes fatigue life in power transmission components, ensuring the outer working surfaces handle intense sliding friction while the core withstands cyclic shock.
Standard 8620 Heat Treatment Temperature Ranges
Are improper thermal steps compromising your component performance? Getting the full structural benefits of 8620 material requires tight temperature control across every processing phase. We follow exact temperature windows during thermal processing to guarantee high surface wear resistance alongside reliable core ductility:
- Forging / Thermal Processing (1150°C – 1200°C): Uniform soaking within this range ensures smooth material flow and eliminates structural voids during hot working.
- Normalizing (870°C – 900°C): Controlled air cooling refines the grain size and homogenizes the microstructure after casting or forging.
- Carburizing (880°C – 930°C): This primary 8620 heat treatment carburizing phase diffuses carbon into the outer layer to establish a deep, wear-resistant case profile.
- Quenching (820°C – 850°C): An immediate oil quench transforms the carbon-rich surface into a high-hardness martensite structure while keeping the core tough and ductile.
- Tempering (150°C – 200°C): A low-temperature hold relieves severe quenching strains and reduces brittle fracture risks without sacrificing surface hardness.
By strictly auditing furnace atmospheres and cycle times at each stage, we deliver predictable, repeatable metallurgical properties across every 8620 alloy steel part we produce.
Process Control for 8620 Material Investment Castings
Dimensional variation between batches, shell defects, and chemistry drift can ruin a production run. We eliminate these risks by running automated equipment and strict process controls at every stage of our foundry operations.
How We Guarantee Consistency in 8620 Alloy Steel
- Automated Hydraulic Wax Injection: Pattern consistency drives final casting accuracy. Our hydraulic wax injection machines precisely control temperature, pressure, and dwell time, ensuring zero shrinkage variation and repeatable pattern dimensions across every production run.
- Automated Shell Coating & Steam Dewaxing: Robotic dipping lines build ceramic shells with uniform wall thickness and optimal permeability. High-pressure steam dewaxing autoclaves quickly melt out the wax without stressing the ceramic walls, preventing cracking and flash defects in the final 8620 material components.
- Spectrographic Melt Analysis Prior to Pouring: We take molten samples directly from the induction furnace for real-time optical emission spectroscopy before every single pour. This step verifies that the carbon, nickel, chromium, and molybdenum levels meet exact 8620 steel chemistry specifications before the metal enters the mold.
Scalable Production and Machining for 8620 Material
How do you bridge the gap between initial prototyping and full-scale OEM supply?
We manage your entire manufacturing lifecycle under one roof. Whether you need a short prototyping run to test a new component design or full-scale OEM manufacturing exceeding 200,000+ units per year, our facility handles your 8620 material castings with complete dimensional repeatability.
By combining precision investment casting with full in-house secondary machining, we eliminate multi-vendor handoffs, shrink lead times, and maintain absolute quality control over every part.
In-House Machining & Finishing Capabilities
- Flexible Production Runs: Seamless scaling from rapid prototyping batches to high-volume OEM assembly lines.
- Precision CNC Milling & Turning: Multi-axis CNC machining centers achieve tight tolerances on complex geometries, reducing raw material waste.
- Surface & Cylindrical Grinding: Dedicated grinding operations meet strict surface finish specs and tight journal dimensions on 8620 steel shafts and gears.
- Surface Treatments & Preparation: Integrated shot blasting, passivating, and surface cleaning designed specifically for post-casting heat treatment and case hardening.
Global 8620 Material Equivalents
Sourcing components internationally often creates friction when cross-referencing regional steel standards. How do you ensure foreign foundries deliver exact metallurgical matches for your engineering prints?
We manufacture and pour 8620 material to match major international cross-reference standards, guaranteeing complete mechanical and chemical interchangeability for global supply chains.
| Country / Standard | Designation / Standard Code | Equivalent Grade |
|---|---|---|
| United States (AISI/SAE) | AISI 8620 / SAE 8620 | UNS G86200 |
| Germany / Europe (DIN/EN) | DIN 1.6523 | 20NiCrMo2-2 / EN362 |
| Japan (JIS) | JIS SNCM220 | SNCM220H |
| United Kingdom (BS) | BS 805M20 | EN362 |
Supply Chain Interchangeability
- Exact Chemical Match: Whether your prints call out a DIN 1.6523 equivalent or JIS SNCM220 material, we strictly control melt chemistries to guarantee cross-standard compliance.
- Zero Substitution Risk: We provide full Mill Test Reports (MTRs) certifying chemistry and mechanical properties to AISI 8620 alloy steel and UNS G86200 properties with every shipment.
- Uniform Heat-Treat Processing: All cross-referenced grades maintain identical carbon absorption rates during carburizing, ensuring consistent case depths and core ductility regardless of sourcing origin.
Typical Applications for Cast 8620 Components
Where does 8620 material perform best when high impact, surface wear, and fatigue resistance are non-negotiable? We cast and heat-treat 8620 alloy steel for critical applications requiring a hard, wear-resistant outer shell combined with a shock-absorbing core.
Automotive & Drive Systems
Power transmission parts demand high fatigue strength to withstand continuous torque and impact loads: Gears & Pinions: Case-hardened surface prevents tooth wear while the ductile core absorbs heavy shock. Crankshafts & Ring Gears: Maintains tight dimensional tolerances under thermal and mechanical stress. Spline Shafts: Delivers high torsional fatigue resistance and smooth surface interaction.
Heavy Industrial Machinery
For heavy equipment facing aggressive abrasion and heavy payloads, components cast from 8620 steel optimize service life: Bushings & Wear Plates: Resists continuous sliding friction and galling. Chain Pins & Valve Bodies: Handles cyclic mechanical stress and pressure surges without cracking.
Aerospace & Defense
High-stress, mission-critical hardware requires extreme structural reliability: Structural Brackets & Fasteners: High strength-to-weight efficiency produced near-net-shape via 8620 steel investment casting. High-Impact Wear Fittings: Retains high fracture toughness under extreme dynamic loading.
Oil & Gas / Mining
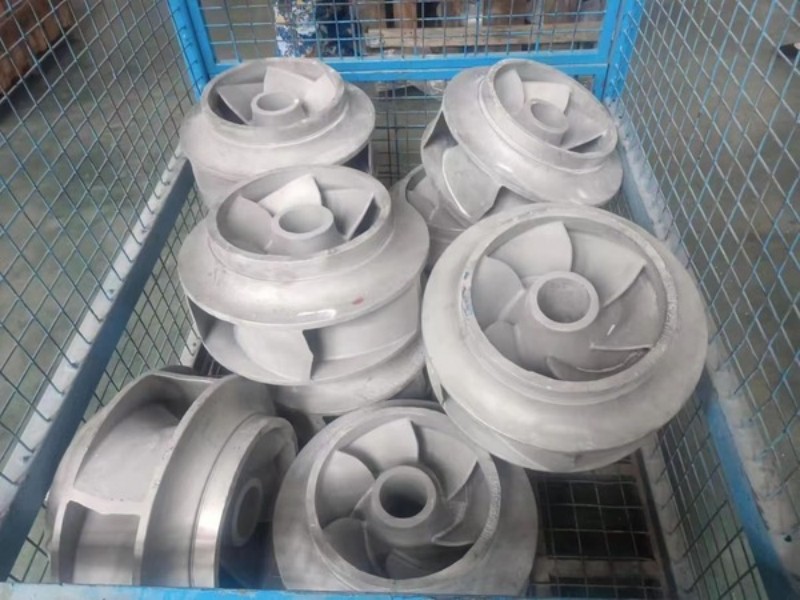
Abrasive downhole and drilling conditions require localized extreme surface hardness: Rock Drill Bits: Withstands harsh rock face impact and continuous abrasive erosion. Pump Components & Connector Sleeves: Maintains structural integrity under high pressure and shock-loaded fluid flow.
Quality Control for 8620 Material
How do you verify that your cast alloy components will hold up under heavy wear and match tight engineering drawing tolerances? We eliminate guesswork through strict quality controls, full heat-number traceability, and complete testing at every stage of casting and machining.
- ISO 9001 Quality System: Our entire workflow operates under an ISO 9001 certified quality management system to guarantee consistent quality across every production lot.
- On-Site Chemical Verification: We run optical emission spectrographic melt testing on every liquid batch prior to pouring, ensuring your 8620 material meets exact chemical composition standards.
- CMM Dimensional Inspection: High-precision Coordinate Measuring Machines verify critical dimensions directly against your native 3D CAD models.
- Non-Destructive Testing (NDT): We perform Dye Penetrant Inspection (DPI) and Magnetic Particle Inspection (MPI) to detect any surface or subsurface discontinuities before parts ship.
- Full Material Traceability: Every shipment includes comprehensive Mill Test Reports (MTRs) tied directly to individual heat numbers, providing complete chemical and mechanical certification.
Frequently Asked Questions About 8620 Material
Is 8620 steel hardenable through-and-through?
No. The 8620 material is a low-carbon alloy designed specifically as a case-hardening steel. Due to its low carbon content (0.18%–0.23%), standard quenching will not harden the material through its entire cross-section. Instead, carburizing heat treatment adds carbon to the outer layer, delivering high surface hardness (58–62 HRC) while preserving a ductile, shock-resistant core (30–40 HRC).
How does 8620 compare to 4140 alloy steel?
While both are popular engineering alloys, their carbon levels dictate different processing methods and mechanical uses:
- 8620 Alloy Steel: Low-carbon case-hardening grade (0.18%–0.23% C). Optimized for high surface wear resistance combined with deep core toughness. Ideal for gears, pinions, bushings, and impact loads.
- 4140 Alloy Steel: Medium-carbon through-hardening grade (0.38%–0.43% C). Achieves uniform strength and hardness across the entire cross-section. Ideal for high-tensile shafts, heavy bolts, and structural components.
Can VastPCC supply finished machined 8620 castings?
Yes. We provide complete, turn-key manufacturing for cast components. We handle the entire process in-house—from investment casting and heat treating to secondary CNC milling, turning, and precision grinding. Every shipment arrives ready for assembly, backed by complete CMM dimensional reports and heat-number material traceability.


 English
 Russian
 German