
2026年8月29日
Learn what austenitic stainless steel is with FCC structure nonmagnetic properties grades and applications
What is Austenitic Stainless Steel?
Selecting the right alloy for environments requiring superior corrosion resistance, high ductility, and non-magnetic performance can be challenging. Austenitic stainless steel is the most widely specified class of stainless steel, defined metallurgically by a face-centered cubic (FCC) crystalline lattice (gamma-phase iron). Unlike standard ferritic or martensitic steels, this unique atomic structure remains thermodynamically stable from cryogenic temperatures up to extreme industrial heating zones.
Face-Centered Cubic Structure Mechanics
The core mechanical and physical performance of austenitic alloys stems directly from their distinct atomic geometry:
- Atomic Packing Efficiency: Atoms reside at eight corners and six face centers of a unit cube, providing a high atomic packing factor (0.74).
- Cryogenic Ductility: Multidirectional slip systems within the FCC lattice prevent ductile-to-brittle transition, preserving impact toughness at temperatures below -196°C.
- Non-Magnetic Profile: The symmetrical FCC lattice yields zero intrinsic magnetic permeability in the fully solution-annealed condition.
The Role of Austenite Stabilizers
To suppress ferrite formation and lock in the FCC structure during solidification, we optimize alloy chemistry using key stabilizing elements:
| Stabilizing Element | Metallurgical Function | Processing Advantage |
|---|---|---|
| Nickel (Ni) | Expands the gamma phase field; prevents phase transformation | Maximizes grain stability and deep-drawing ductility |
| Manganese (Mn) | Replaces nickel; increases matrix solubility for nitrogen | Enhances hot-workability while maintaining cost efficiency |
| Nitrogen (N) | Potent interstitial strengthener; improves pitting resistance | Elevates yield strength without sacrificing toughness |
Industrial Dominance (~70% Global Market Share)
Austenitic grades account for approximately 70% of global stainless steel manufacturing. Their unmatched balance of formability, weldability, and environmental resistance makes them the primary specification for critical applications.
Harnessing these metallurgical fundamentals requires strict thermal and chemical control. At Vastpcc, we utilize automated shell molding and precision induction melting to produce complex austenitic investment castings, setting the industry benchmark for tight dimensional tolerances, controlled phase balance, and zero micro-porosity under ASTM and ISO standards.
Chemical Composition of Austenitic Stainless Steel
When engineering high-performance components, understanding what is austenitic stainless steel comes down to balancing fundamental chemical mechanics. We formulate these alloys around a precise core matrix of chromium and nickel, systematically modified with targeted secondary additives to satisfy stringent ASTM and ISO specifications.
Core Elemental Balance
- Chromium (16%–26%): Forms a dense, self-healing chromium oxide passive film across the surface, providing primary oxidation and atmospheric corrosion resistance.
- Nickel (6%–22%): Acts as the primary austenite stabilizer, converting the crystal lattice into a face-centered cubic structure while expanding impact toughness and ductility.
Secondary Alloying Additives
To refine mechanical performance for hostile processing environments, we integrate specific secondary elements into our austenitic stainless steel properties matrix:
- Molybdenum (2%–7%): Significantly elevates resistance to localized pitting and crevice corrosion in high-chloride and acidic environments.
- Titanium / Niobium: Functions as strong carbide formers that tie up free carbon, stabilizing the alloy against intergranular cracking during high-temperature service.
- Nitrogen: Increases yield strength through interstitial solid-solution strengthening while enhancing pitting resistance without sacrificing phase stability.
Standard vs. Low-Carbon ("L") Grades
During thermal cycles or welding between 450°C and 850°C, carbon in standard-grade alloys binds with chromium to form chromium carbides along grain boundaries. This localized chromium depletion leaves the matrix vulnerable to intergranular corrosion.
To eliminate this sensitization mechanism in our custom cast stainless steel alloys, we utilize low-carbon variants designated with an "L" suffix.
| Alloy Variant | Carbon Content | Sensitization Susceptibility | Primary Engineering Advantage |
|---|---|---|---|
| Standard (e.g., 304, 316) | ≤ 0.08% Max | Moderate to High during welding | Higher allowable stress at elevated temperatures |
| Low Carbon (e.g., 304L, 316L) | ≤ 0.03% Max | Extremely Low / Negligible | Superior as-welded intergranular corrosion resistance |
Classification of Austenitic Stainless Steel Families
Understanding what is austenitic stainless steel requires categorizing its structural families based on chemical formulation and performance boundaries. We break down these alloys into three core classifications serving global B2B manufacturing needs.
300 Series (Chromium-Nickel Alloys)
The 300 series forms the backbone of global industrial production. These chromium-nickel formulation standards offer superior ductility, excellent weldability, and versatile corrosion performance.
- Grade 304 / 304L: The standard 18/8 alloy balance used for structural hardware, food processing, and high-volume industrial enclosures.
- Grade 316 / 316L: Formulated with 2%–3% molybdenum for enhanced pitting resistance against aggressive chloride environments. Analyze key chemistry variations in our detailed technical review on the difference between 304 and 316 stainless steel.
- Grade 321: Titanium-stabilized to prevent intergranular chromium carbide precipitation during elevated-temperature welding operations.
- Grade 310 / 310S: High-nickel (19%–22%) and high-chromium (24%–26%) composition built specifically for furnace components and thermal processing equipment.
For complete chemical balance metrics, refer to our comprehensive guide on 300 series stainless steel grades.
200 Series (Chromium-Manganese-Nitrogen Alloys)
The 200 series replaces a significant portion of nickel with manganese and nitrogen to deliver a cost-effective material alternative. These 200 series manganese alloys preserve the non-magnetic, face-centered cubic structure while optimizing raw material expenditure.
- High Tensile Yield: Delivers higher yield strength than standard 300 series alloys due to interstitial nitrogen strengthening.
- Target Applications: Well-suited for indoor architectural trim, structural transport framing, and moderate-exposure hardware.
Super Austenitic Steel Alloys
Engineered for severe chemical environments, super austenitic steel contains high nickel (20%–25%), elevated chromium (20%–27%), and heavy molybdenum additions (6%–7%).
- Pitting Resistance: Achieves Pitting Resistance Equivalent Numbers (PREN) exceeding 42 for severe chloride exposure.
- Acid Handling: Provides exceptional service life in hot sulfuric, phosphoric, and aggressive organic acid processing systems.
- Industrial Footprint: Essential for offshore oil extraction platforms, flue-gas desulfurization (FGD) scrubbers, and high-purity chemical processing equipment.
Physical, Mechanical, and Corrosion Properties of Austenitic Stainless Steel
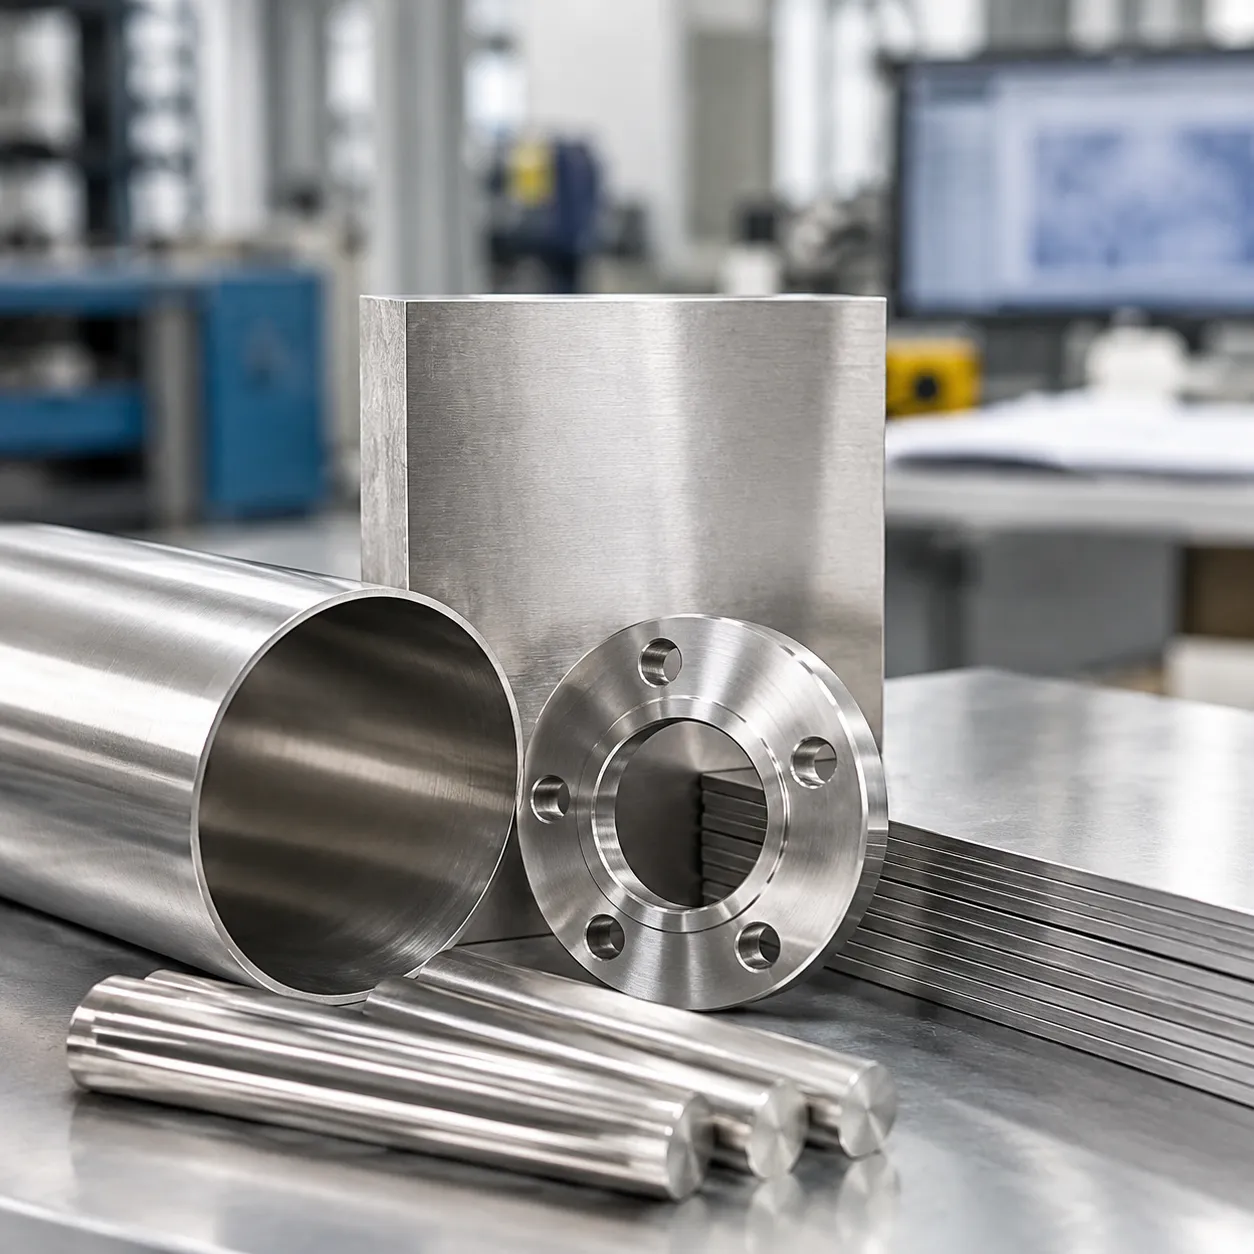
To understand what is austenitic stainless steel capable of under extreme operational stress, we analyze its physical, mechanical, and chemical profile. Its stable crystal lattice provides exceptional ductility, broad thermal tolerance, and high corrosion resistance across demanding industrial settings.
Magnetic Behavior: Annealed vs. Cold-Worked States
In its fully solution-annealed state, austenitic stainless steel remains completely non-magnetic due to its face-centered cubic (FCC) crystal structure. Mechanical strain during processing alters this state:
- Solution-Annealed State: Non-magnetic response with a relative magnetic permeability (μ_r) near 1.0.
- Cold-Worked State: Plastic deformation induces a partial phase transformation from austenite to ferromagnetic martensite, introducing localized magnetic attraction.
- Thermal Restoration: Re-heating the alloy to solution annealing temperatures (1010°C to 1120°C) followed by rapid quenching restores full austenitic grain stability and eliminates magnetic response.
Cryogenic Toughness and Thermal Creep Resistance
Austenitic alloys do not exhibit a sharp ductile-to-brittle transition temperature, providing predictable mechanical performance from deep freeze to high heat:
- Cryogenic Performance: Retains impact energy absorption exceeding 100 J (Charpy-V notch) down to cryogenic temperatures (-196°C), preventing brittle fracture in liquid gas containment.
- High-Temperature Resistance: Delivers oxidation resistance and high-temperature creep resistance up to 870°C for standard grades and up to 1150°C for high-nickel variants. For severe thermal applications involving combined wear and aggressive scaling, engineers frequently benchmark these properties against cobalt-based castings for heat, wear, and corrosion resistance.
Pitting Resistance Equivalent Number (PREN) Breakdown
We evaluate pitting and crevice corrosion behavior in chloride environments using the Pitting Resistance Equivalent Number (PREN). Higher numbers indicate stronger defense against localized attack.
Mathematical Index: PREN = %Cr + 3.3(%Mo + 0.5%W) + 16(%N)
| Alloy Class | Typical Alloy Balance | PREN Index | Target Environment |
|---|---|---|---|
| Grade 304 | 18% Cr, 0% Mo, 0.10% N | ~19.0 | Fresh water, food processing, structural hardware |
| 316L Marine Grade | 16.5% Cr, 2.1% Mo, 0.05% N | ~23.5–25.0 | Marine environments, chemical handling, pharmaceuticals |
| Super Austenitic | 20% Cr, 6.5% Mo, 0.20% N | ≥ 42.0 | Concentrated acids, flue-gas cleaning, offshore rigs |
Ductility, Work Hardening, and Weldability
The mechanical processing advantages of these alloys stem from three primary characteristics:
- High Ductility: Elongation values consistently exceed 40% to 60%, allowing severe deep drawing and roll forming without intermediate annealing.
- High Work Hardening Rate: Rapidly increases yield strength when deformed, providing structural impact resistance and energy dissipation.
- Weldability: Welds cleanly via TIG, MIG, and submerged arc methods without pre-heating. Utilizing low-carbon variants prevents chromium carbide precipitation along grain boundaries, maintaining intergranular corrosion resistance across heat-affected zones.
Precision Investment Casting of Austenitic Stainless Steel
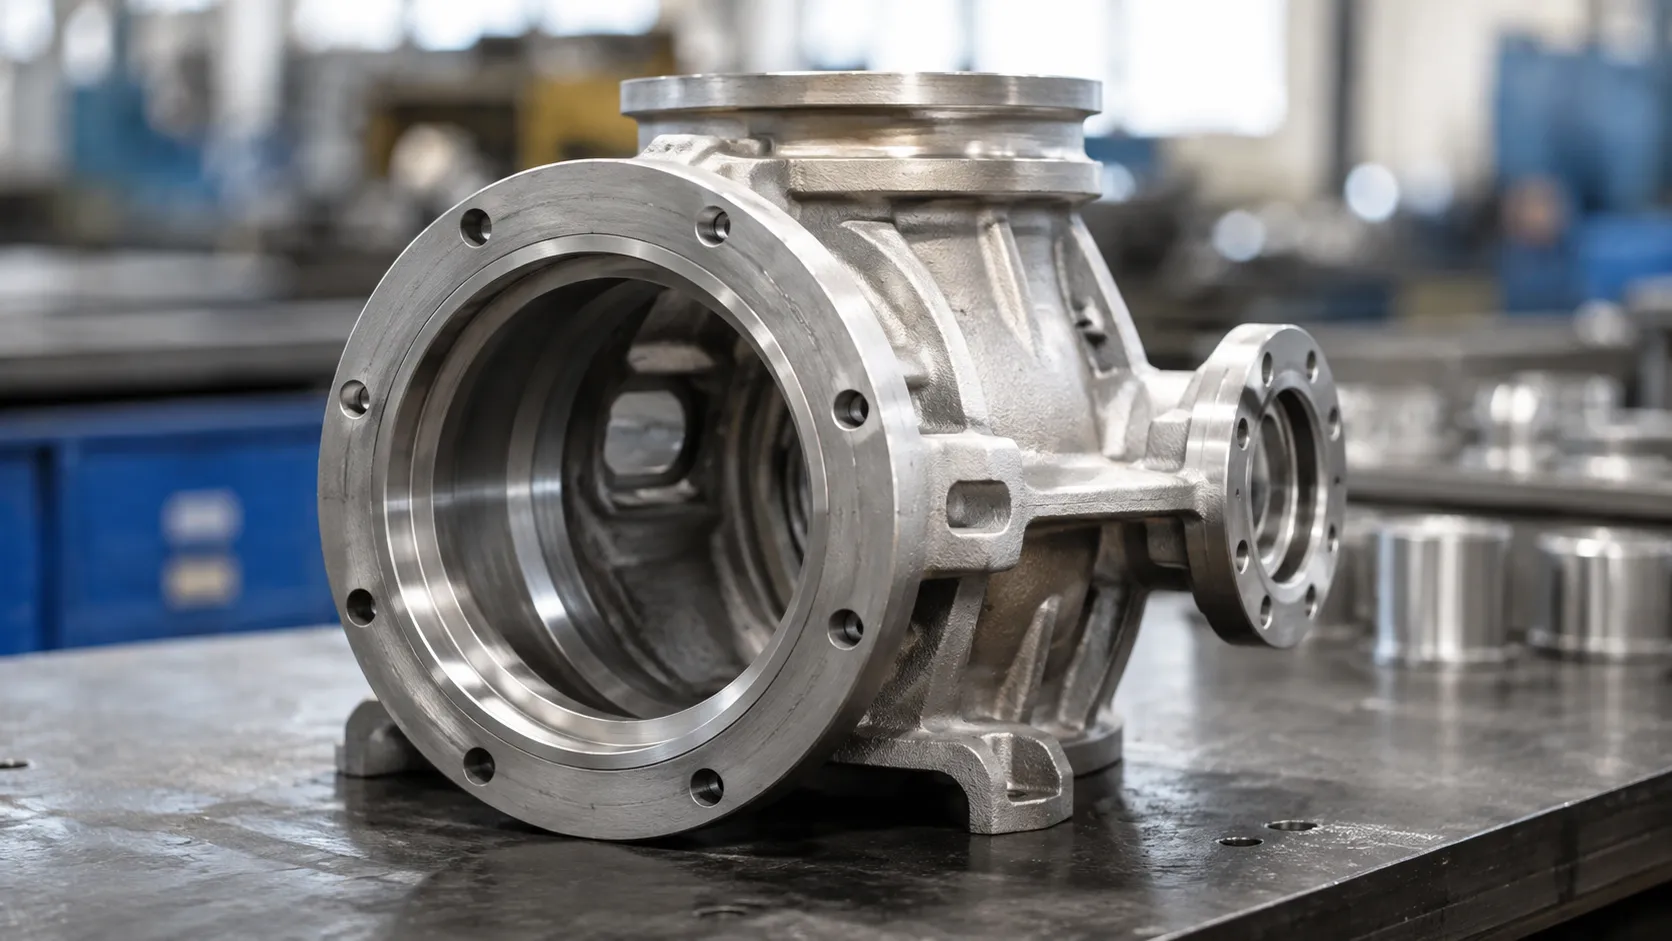
We manufacture complex austenitic stainless steel components using high-precision investment casting engineered for demanding industrial environments. Our end-to-end production workflow guarantees strict metallurgical control, superior surface integrity, and tight dimensional tolerances.
Pattern Production: High-Stability Wax Injection
We utilize temperature-controlled, high-stability wax injection machinery to fabricate sacrificial patterns. This eliminates dimensional distortion and thermal shrinkage, providing an exact physical baseline for complex high-alloy geometries.
Shell Mold Preparation & Coating
Automated coating cells execute multi-layer slurry dipping and stucco application. To deliver exceptional surface finish and structural mold integrity, we utilize our precision casting solution with silica sol process and ISO 8062 accuracy alongside automated marking protocols for batch traceability.
High-Pressure Dewaxing Autoclaves
Ceramic-coated assemblies undergo flash dewaxing inside high-pressure steam autoclaves. Rapid pressurization prevents wax expansion stress, eliminating ceramic shell micro-cracking and preserving core mold integrity prior to high-temperature firing.
Induction Melting & Controlled Pouring
We melt austenitic alloys using medium-frequency induction furnaces with argon gas cover. This prevents chromium and manganese burn-off while minimizing oxide inclusion entrapment during pouring.
- Melting Temperature Range: 1420°C to 1480°C
- Atmospheric Control: Inert gas purging to preserve alloy chemistry balance
- Degassing: Vacuum/inert gas degasification for micro-porosity reduction
Post-Casting Heat Treatment & Passivation
To eliminate carbide precipitation during cooling, castings undergo full solution annealing at 1040°C to 1120°C followed by rapid water quenching. This redissolves intergranular chromium carbides back into the austenitic grain matrix. Subsequent nitric or citric acid passivation removes residual surface free iron.
Process Tolerances with Vastpcc Solutions
Combining high-integrity investment casting with precision post-machining, Vastpcc solutions consistently achieve strict target tolerances across critical structural components.
| Process Metric | Vastpcc Precision Capability |
|---|---|
| Machining Precision | ≤5μm tight-tolerance machining |
| Surface Finish | Ra 1.6–3.2 μm (As-cast) / Ra <0.4 μm (Post-machined) |
| Nondestructive Testing | 100% Radiographic (X-Ray) & Liquid Penetrant Testing (PT) |
| Dimensional Standard | ISO 8062 CT4–CT6 precision casting grades |
Technical Grade Comparison Matrix
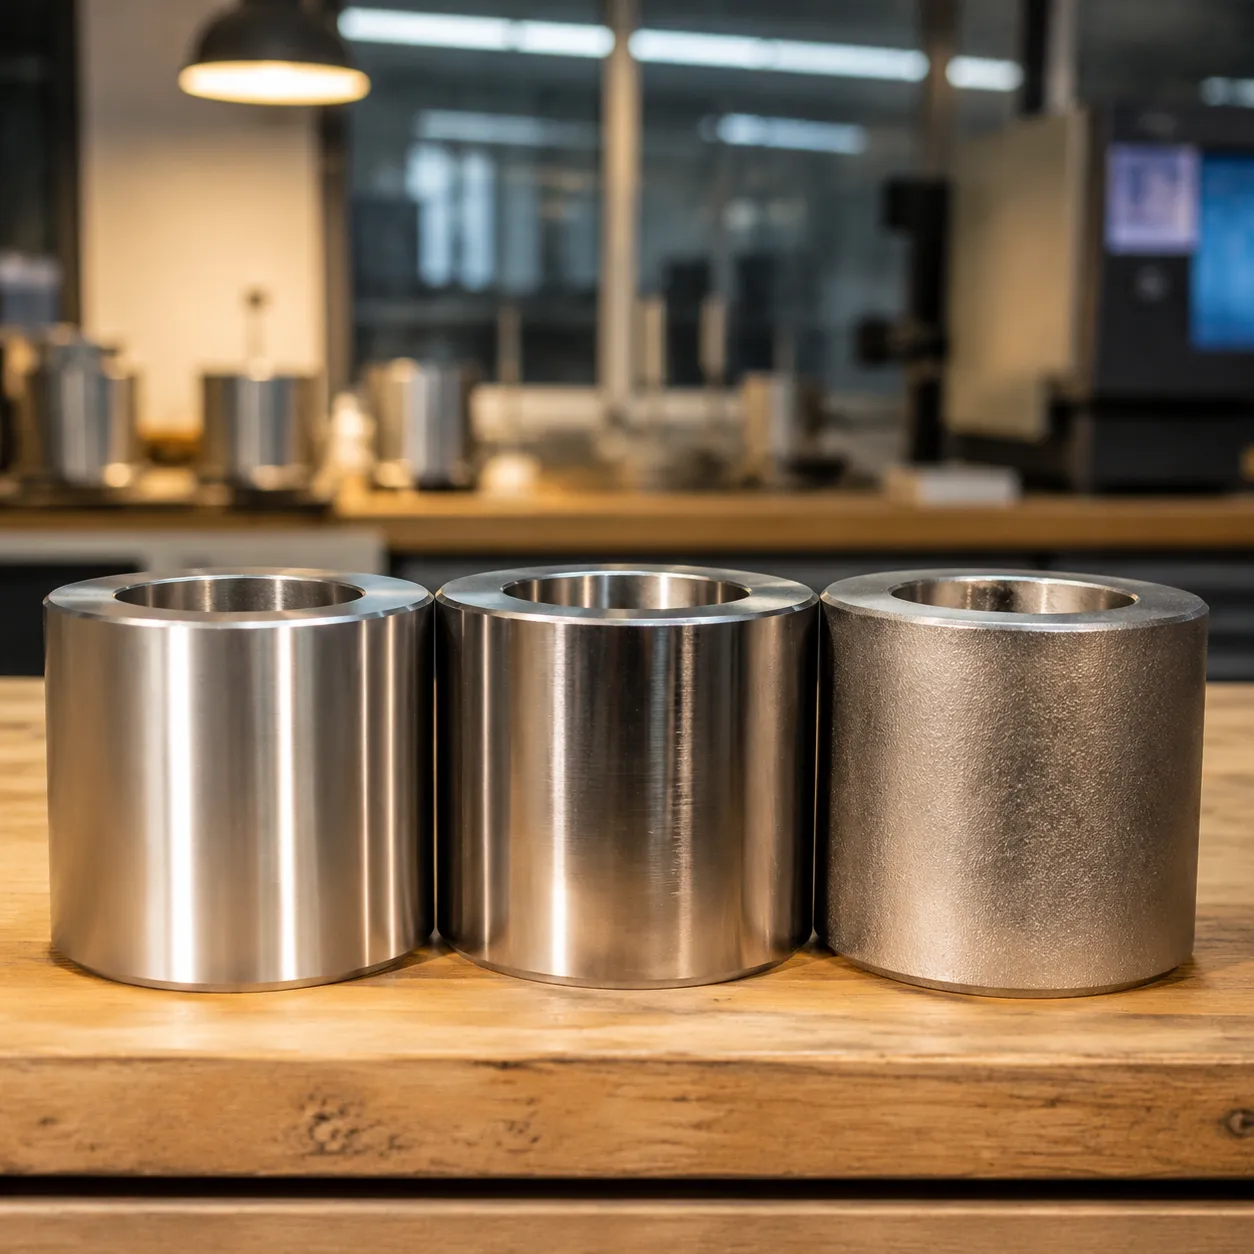
Selecting the right alloy balance dictates operational limits, corrosion performance, and mechanical efficiency. To evaluate what is austenitic stainless steel capable of across aggressive industrial environments, we analyze standard chemical compositions—from baseline 18/8 stainless steel formulations to advanced super austenitic grades. Reviewing our stainless steel casting guide provides additional insight into matching these material compositions with optimal manufacturing processes.
| Stainless Steel Grade | Nominal Composition | Core Metallurgical Properties | Primary B2B Applications |
|---|---|---|---|
| Grade 304 / 304L | 18% Cr, 8% Ni | Baseline 300 series alloy; excellent formability and general corrosion resistance | Structural hardware, food processing, architectural fittings |
| Grade 316 / 316L | 16% Cr, 10% Ni, 2% Mo | 316L marine grade; elevated chloride pitting resistance via molybdenum | Chemical processing, medical implants, marine hardware |
| Grade 310S | 25% Cr, 20% Ni | High-chromium/nickel balance; extreme oxidation and creep resistance | Furnace components, heat exchangers, kiln equipment |
| Grade 321 | 18% Cr, 10% Ni + Ti | Titanium-stabilized alloy; prevents chromium carbide precipitation during welding | Aerospace exhaust manifolds, heavy-duty expansion joints |
| Grade 201 | 16% Cr, 4% Ni, 6% Mn | 200 series manganese alloy; cost-effective alternative with moderate strength | Decorative trim, light structural hardware, transit equipment |
| Grade 904L | 20% Cr, 25% Ni, 4.5% Mo | Super austenitic steel; superior resistance to reducing acids and stress cracking | Sulfuric acid processing, offshore oil rigs, seawater cooling |
- Low-Carbon "L" Variants: 304L and 316L limit carbon content to \le 0.03% to prevent intergranular corrosion in heavy-section weldments.
- Thermal Stabilization: Titanium additives in Grade 321 lock down carbon content, maintaining grain boundary stability between 425°C and 850°C.
- Cost-Optimized Alternatives: Manganese substitution in Grade 201 reduces reliance on nickel while maintaining moderate structural integrity.
- Extreme Acid Resistance: Grade 904L incorporates high copper, nickel, and molybdenum content to withstand harsh chemical environments.
Core Industrial Applications of Austenitic Stainless Steel
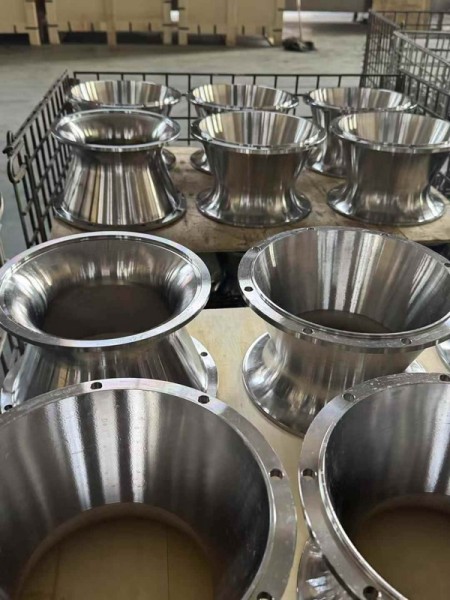
Understanding what is austenitic stainless steel comes down to where it excels: harsh environments requiring exceptional corrosion resistance, cryogenic toughness, and high-temperature stability. We manufacture and supply these alloys across four primary sectors:
Aerospace & Aviation
- Fluid Handling Lines: High-pressure hydraulic lines and fuel manifolds operating under severe thermal cycling and vibration.
- Structural Fittings: High-ductility bracketry and exhaust hardware that resist atmospheric oxidation at elevated temperatures.
Medical & Pharmaceutical
- Surgical Instruments & Enclosures: Non-magnetic tools and device housings that withstand repeated harsh chemical and autoclave sterilization.
- Sanitary Process Equipment: Biopharmaceutical mixing tanks and fluid transfer systems designed with ultra-smooth surfaces to prevent bacterial adhesion.
Petrochemical & Marine
- Corrosive Flow Control: Heavy-duty acid pump housings, valve bodies, and impellers handling aggressive chloride and sulfuric streams.
- Offshore Castings: Submerged hardware made from 316L and super austenitic alloys to withstand continuous saltwater pitting.
Precision Equipment Manufacturing
- Custom OEM Investment Cast Components: Complex OEM hardware, pump impellers, and sensor housings built to micron-level accuracy. Utilizing our high-precision industrial wax equipment for investment casting, we produce dense, near-net-shape components that significantly reduce downstream machining costs for global equipment manufacturers.
Frequently Asked Questions: What Is Austenitic Stainless Steel?
Why is austenitic stainless steel non-magnetic?
Austenitic stainless steel features a face-centered cubic (FCC) crystal structure, which maintains zero net magnetic moment in its fully annealed state. Because the iron atoms are arranged in a symmetrical FCC lattice stabilized by nickel, the phase remains non-magnetic at room temperature.
What is the primary operational difference between Grade 304 and Grade 316?
| Feature | Grade 304 | Grade 316 |
|---|---|---|
| Molybdenum Content | 0% | 2.0% – 3.0% |
| Chloride Resistance | Moderate (Susceptible to pitting) | Superior (Resists pitting & crevice corrosion) |
| PREN Rating | ~18 – 20 | ~23 – 25 |
| Primary Environments | General food processing, architectural, structural | Marine, pharmaceutical, chemical processing |
Can austenitic stainless steel be hardened using thermal heat treatment?
No. Austenitic alloys cannot be hardened by conventional heating and quenching processes because the face-centered cubic phase remains stable from sub-zero temperatures up to the melting point. Hardening is achieved exclusively through cold working (strain hardening), which elevates yield strength and mechanical hardness at the expense of ductility.
How does cold working transform austenite to martensite?
Mechanical deformation at temperatures below the strain-induced transformation threshold forces the FCC gamma-austenite lattice to undergo a shear transition. This structural distortion forms strain-induced alpha-martensite, which increases material hardness and introduces slight ferromagnetic properties to heavily deformed zones.
What equipment is required to produce high-precision austenitic steel investment castings?
At Vastpcc, we deploy specialized foundry systems to eliminate micro-segregation and maintain tight dimensional control:
- Pattern & Shell Processing: High-pressure hydraulic wax injectors combined with robotic dipping stations. We integrate advanced automation in the casting process for high-precision investment castings to ensure uniform ceramic shell thickness and structural integrity.
- Dewaxing & Melting: High-pressure steam autoclaves for clean binder removal, coupled with medium-frequency induction melting furnaces operating under controlled atmospheric parameters.
- Heat Treatment & Passivation: Solution annealing furnaces engineered for rapid water quenching at temperatures exceeding 1040 degrees Celsius, followed by chemical passivating baths.
As a certified steel casting manufacturer for custom alloy castings, our processing control guarantees exact chemistry verification and defect-free microstructures across all produced components.


 English
 Russian
 German